How to Choose the Right Shield Gas and MIG Wire Combo for Heavy Fabrication
August 2, 2026 6:30 pm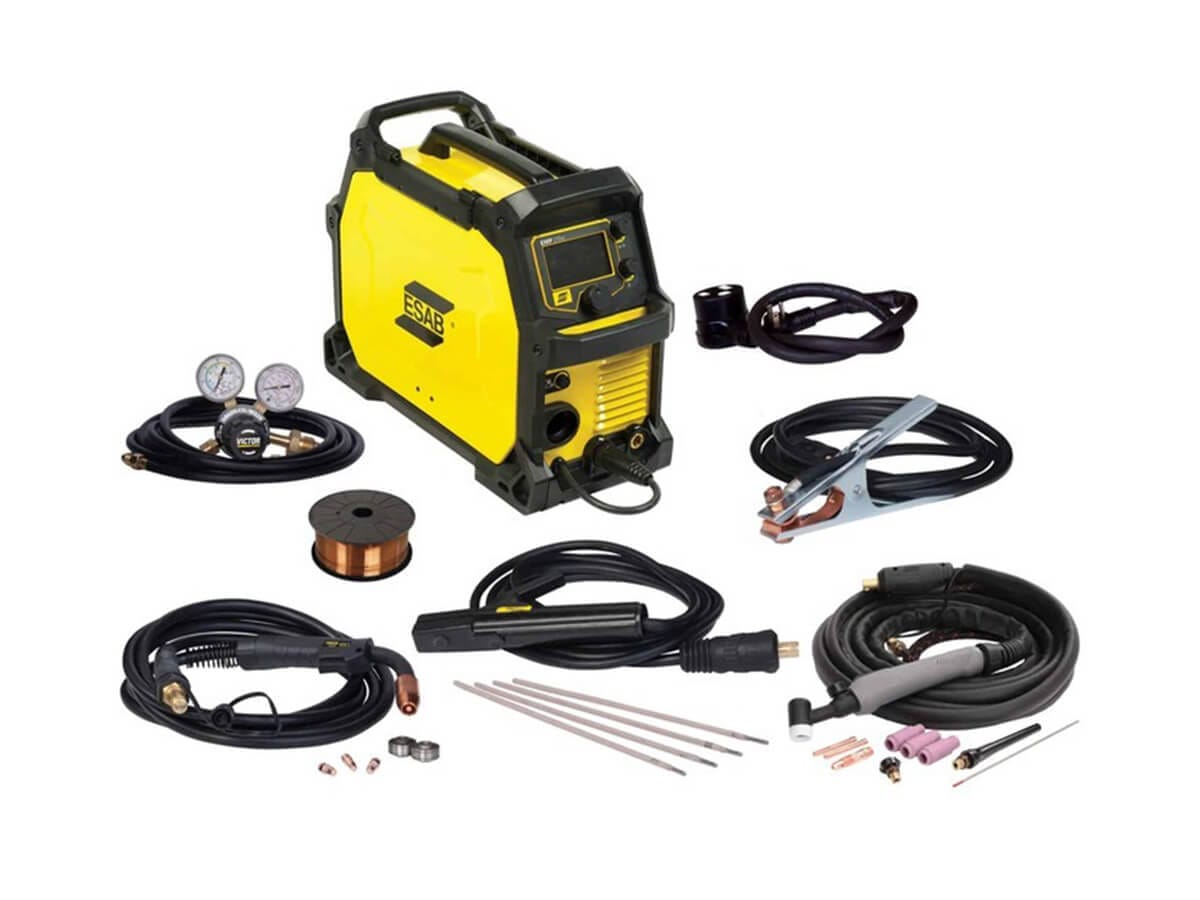
Choosing the proper combination of MIG welding wire and shielding gas determines the strength, appearance, and integrity of heavy fabrication welds. Thick structural steel, heavy machinery, and structural beams require deep penetration, clean metal transfer, and minimal spatter. Pairing solid or flux-cored wire with the correct gas mixture prevents porosity, reduces cleanup time, and ensures full-penetration joints on heavy metal components. Fabricators in Southern Ontario rely on high-performance equipment and industrial shielding blends to meet strict structural code requirements. Selecting appropriate wire diameters, alloy grades, and gas ratios keeps heavy industrial projects running efficiently and safely.
According to industry research from the CWB Group, fabricated metal product manufacturing generates over $16 billion for the national economy, with structural safety depending heavily on proper joining standards. When working with heavy-gauge plate, using incorrect consumables leads to weld defects, costly re-work, and potential structural failure. Sourcing high-grade welding supplies and industrial gases allows local shops to maintain strict quality control across every project. Shops also rely on reliable propane in Toronto to operate pre-heating torches and heavy machinery around the job site.
How to Select the Proper Shielding Gas for Thick Steel Plate
- High-argon gas mixtures for spray transfer
Heavy plate fabrication requires a stable spray arc transfer to achieve deep sidewall fusion. Mixing 85 to 90 percent argon with carbon dioxide creates a smooth arc with minimal spatter. Local shops sourcing welding gas in Toronto, GTA rely on these precise argon mixtures for consistent structural joints.
- Pure carbon dioxide for maximum penetration
Carbon dioxide delivers the deepest joint penetration on thick carbon steel plates. While it creates more surface spatter than argon blends, it provides exceptional heat input at low cost. Fabricators often pair CO2 with robust welding supplies and industrial gases to handle heavy structural beam connections reliably.
- Argon and helium blends for heavy aluminium
Heavy aluminium fabrication demands high heat input due to rapid thermal dissipation in thick sections. Adding helium to argon increases arc temperature, improves puddle fluidity, and reduces pre-heating times. Shops running plasma cutters and pre-heaters powered by propane in Toronto benefit from helium-argon gas blends on thick plate.
- Tri-mix gases for heavy stainless steel
Stainless steel fabrications require precise gas chemistry to maintain corrosion resistance and bead profile. Helium-based tri-mix gases containing argon and carbon dioxide keep puddle fluidity high and prevent carbide precipitation. Securing certified welding supplies and industrial gases guarantees gas purity levels necessary for critical pressure vessel construction.
- Gas flow rate settings for heavy currents
High-amperage MIG welding generates strong thermal plumes that disrupt shielding gas coverage. Setting gas flow rates between 35 and 45 cubic feet per hour protects the molten weld pool from atmospheric contamination. Ordering high-capacity cylinders of welding gas in Toronto, GTA prevents sudden pressure drops during continuous production runs.
- Regulators and flow meters for stable gas delivery
Maintaining steady gas flow requires heavy-duty dual-stage regulators and clear flow meters. Fluctuations in line pressure cause porosity and internal oxidation in heavy welds. Top-tier welding supplies and industrial gases include specialized high-flow regulators built to handle demanding multi-shift manufacturing environments without freezing or drifting.
Call Josef Gases at (416) 658-1212 to discuss customized gas cylinder deliveries and high-flow regulator setups for your facility.
Choosing MIG Wire Types and Diameters for Heavy Welds
- Solid wire ER70S-6 for dirty or rusty plate
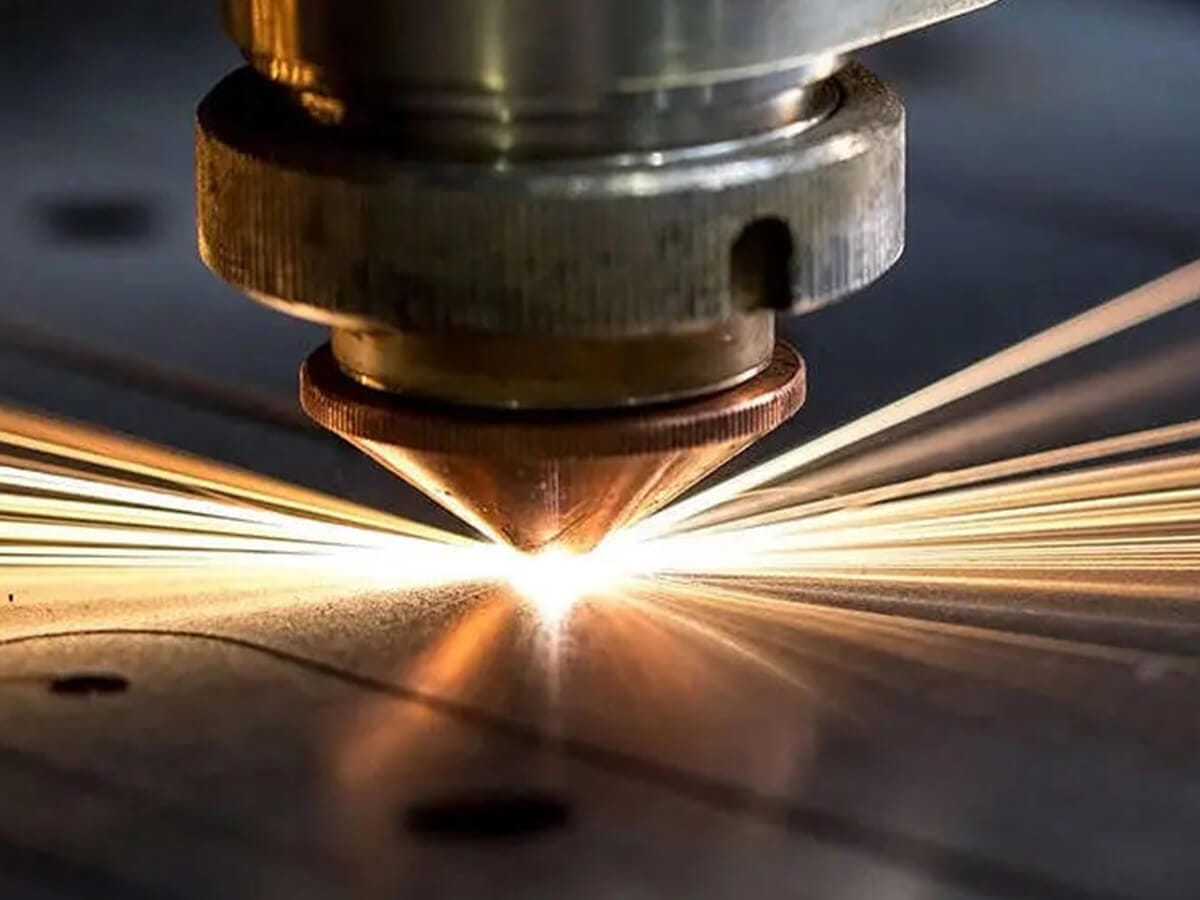
Solid ER70S-6 wire contains higher levels of silicon and manganese deoxidizers than ER70S-3 wire. These additions help weld through light mill scale, rust, and surface impurities on heavy plate. Fabricators sourcing premium wire alongside welding gas in Toronto, GTA achieve smooth arc stability and cleaner weld beads.
- Gas-shielded flux-cored wire for maximum deposition
Dual-shield flux-cored wire combines an internal flux with external shielding gas to deposit metal rapidly. It excels at multi-pass welds on thick structural steel sections. Equipping your workshop with high-performance welding supplies and industrial gases ensures your dual-shield wire produces slag that peels away effortlessly after welding.
- Thick wire diameters for deep joint filling
Selecting 1.2 millimetre or 1.6 millimetre wire diameters allows welders to carry high current levels without burn-through. Thick wire fills large, bevelled joints quickly, reducing total labour hours per job. Facilities using fuel torches powered by propane in Toronto for bevel preparation pair heavy wire with high-amperage guns.
- Metal-cored wire for high-speed production
Metal-cored wire offers high deposition rates without producing heavy slag layers, making it ideal for robotic or semi-automatic heavy fabrication. It provides broad joint penetration profiles and minimal spatter. Purchasing top-tier welding supplies and industrial gases ensures consistent wire chemistry, preventing wire feeding interruptions on automated lines.
- Submerged arc consumables for ultra-thick sections
Ultra-heavy plate above two inches thick often requires submerged arc wire and granular flux systems. This process delivers extreme deposition rates with zero open arc flash. Using reliable welding gas in Toronto, GTA for tack welding before submerged arc welding keeps heavy assemblies aligned prior to final passes.
- Drive rolls and liner selection for thick wires
Heavy MIG wire requires exact drive roll knurling and Teflon or steel liners to prevent feeding friction. Knurled rolls grip flux-cored wire without crushing it, while smooth V-groove rolls suit solid wire. Upgrading to industrial welding supplies and industrial gases includes matching feed rolls and torch liners precisely.
Best Practices for Setting Up MIG Welding Equipment and Pre-Heat Systems
- Matching wire feeder drive tension
Setting proper drive roll tension prevents wire slipping and bird-nesting at the feeder. Oversized heavy wire needs firm, even pressure to push through long torch cables without stalling. Sourcing heavy-duty feeders along with high-grade welding gas in Toronto, GTA guarantees smooth wire delivery during continuous high-amperage welding operations.
- Pre-heating thick steel sections with fuel gas
Heavy structural steel absorbs heat quickly, raising the risk of cold cracking and brittle weld zones. Pre-heating steel plates to specified temperatures removes moisture and slows cooling rates. Utilizing bulk propane in Toronto for heavy heating torches provides high heat output needed to bring thick plates to target temperatures.
- Selecting water-cooled MIG guns for high amperage
Continuous high-amperage welding on heavy plate overheats standard air-cooled MIG guns within minutes. Water-cooled guns circulate liquid coolant through the handle and conductor tube, extending nozzle life and welder comfort. Equipping production floors with robust welding supplies and industrial gases keeps heavy-duty water-cooled torches running reliably during peak production schedules.
- Joint preparation and bevel grinding techniques
Proper V-groove or U-groove bevel preparation ensures full joint penetration on thick steel plates. Removing heavy scale and grease before welding prevents internal gas entrapment and porosity. Operations running torches with propane in Toronto clean bevel edges thoroughly before applying root passes with high-penetration wire and shielding gas combinations.
- Optimizing contact tip to work distance
Maintaining a contact-tip-to-work distance between 15 and 20 millimetres stabilizes spray transfer arcs on heavy steel. Holding the torch too close causes spatter accumulation inside the gas nozzle, choking gas flow. Ordering premium nozzles and contact tips through suppliers of welding gas in Toronto, GTA maintains clean shielding coverage.
- Managing ground clamp placement and arc blow
High DC welding currents create strong magnetic fields that cause arc blow on thick steel structures. Placing heavy-duty ground clamps directly on the workpiece near the weld joint stabilizes the arc path. Professional welding supplies and industrial gases include high-clamping-force brass grounds designed to carry high currents without overheating.
Selecting the correct shielding gas and MIG wire combination directly influences weld strength, shop productivity, and structural safety on heavy fabrication projects. Matching solid or flux-cored wire chemistry with argon or carbon dioxide blends ensures deep penetration, clean profiles, and minimal cleanup. Investing in high-grade welding guns, feed rolls, and gas regulators supports continuous operation under heavy workloads.
Josef Gases supplies complete lines of compressed gases, high-purity shielding blends, bulk fuel, and professional welding machinery across Southern Ontario. Whether you need reliable welding gas in Toronto, GTA, premium wire feeders, or bulk propane in Toronto, our technical team provides prompt site deliveries and expert support. Contact Josef Gases today at (416) 658-1212 to speak with an industrial specialist and order your welding supplies and industrial gases.