Why is Your Weld Porous? How Gas Flow, Nozzle Wear, and Draft Affect Weld Quality
August 10, 2026 6:50 pm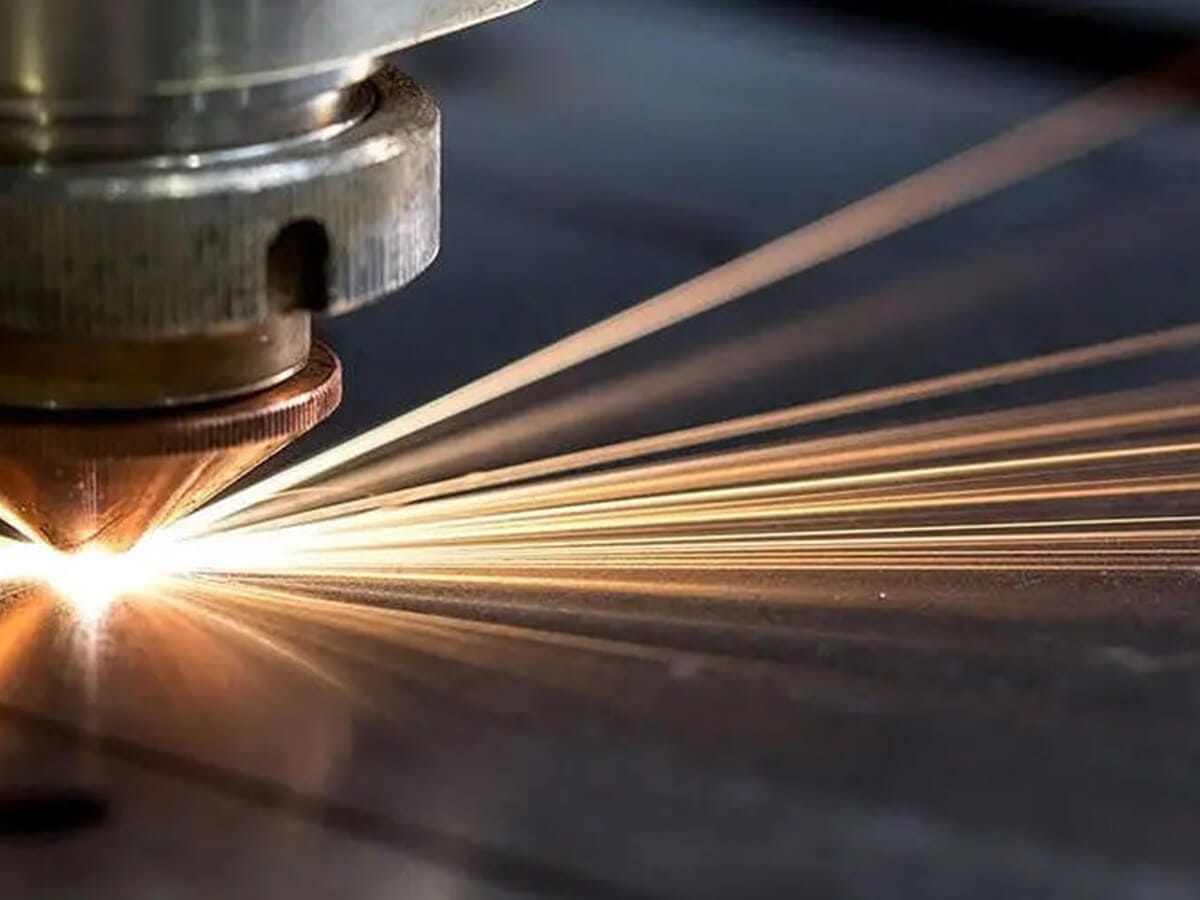
Weld porosity happens when atmospheric air gets trapped inside molten metal, creating tiny pinholes that ruin structural strength. Gas flow shifts, damaged torch parts, and outdoor air currents regularly pull oxygen and nitrogen straight into the open weld pool.
Fixing these issues requires clear troubleshooting habits, clean setup practices, and dependable welding equipment in Toronto. According to the Canadian Welding Bureau (CWB Group), shielding gas coverage issues remain a primary contributor to structural porosity, as little as a 1.5% atmospheric air leak into a gas stream can create severe surface-breaking pores that fail inspection.
Gas Flow Errors and Shield Breakdown
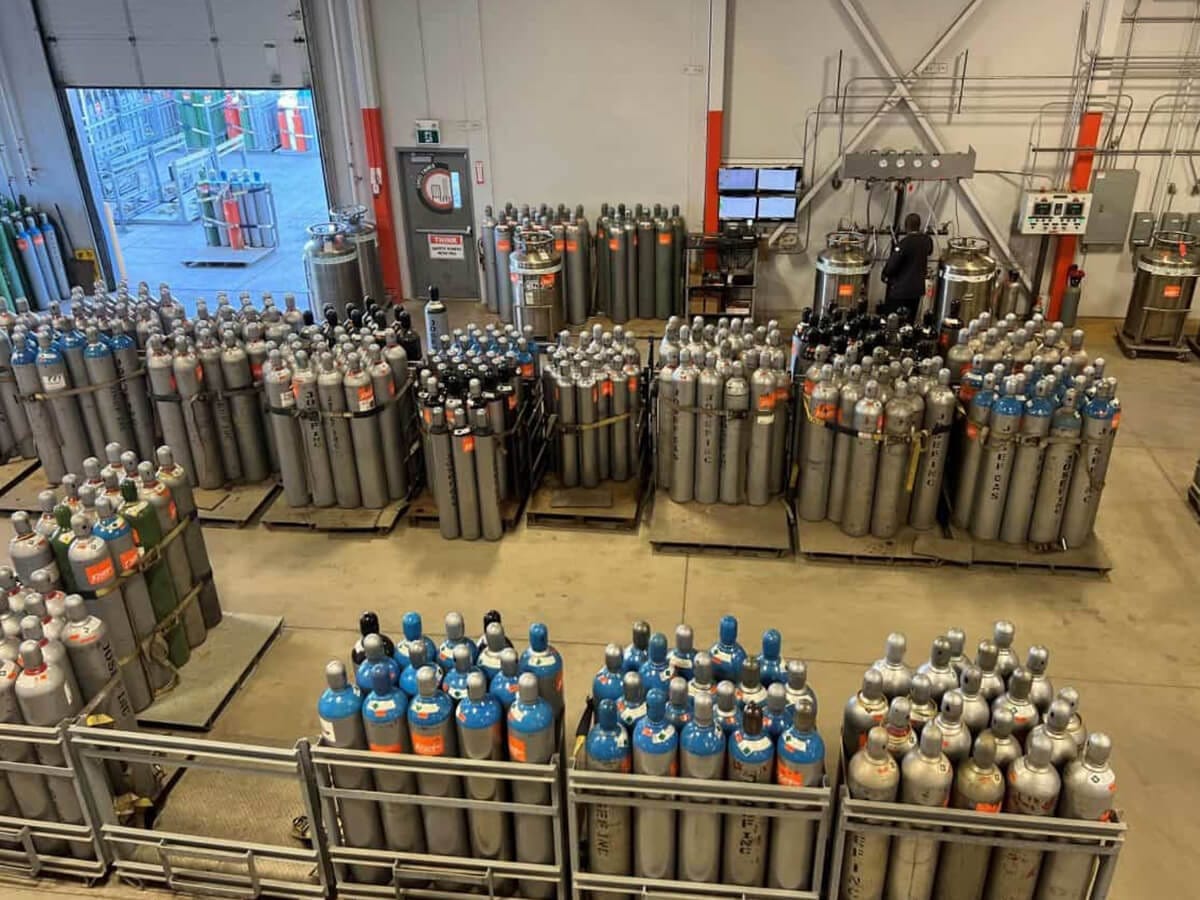
Shielding gas protects the molten puddle from surrounding air. Incorrect pressure or flow rates disrupt this protective envelope and pull atmospheric oxygen and nitrogen directly into the liquid metal.
- Fix excessive cylinder pressure surges: High initial surge pressures turbulence the gas envelope instantly. Installing a dual-stage flowmeter regulator maintains a steady output volume from start to finish.
- Eliminate low flow rate issues: Flow settings below recommended levels leave room for atmospheric air to seep into the arc zone. Adjust gas output according to wire diameter and joint layout.
- Prevent turbulent gas velocity: Cracking open the flowmeter too high creates a fast-moving jet that draws room air into the weld zone. Keep flow rates within balanced operating parameters.
- Inspect hoses for tiny leaks: Cracked lines or loose fittings draw air into the gas line via vacuum effects. Test all torch connections with an approved leak-detection spray.
- Match gas blends to materials: Using straight carbon dioxide on sensitive alloys causes excessive oxidation and porosity. Sourcing specialized welding gas in Toronto guarantees your gas mixture matches your precise material grade.
- Purge supply lines before striking: Trapped air inside a long hose line contaminates the initial inch of your weld bead. Flush gas lines for a few seconds before pulling the trigger.
Need higher grade shielding mixtures or specialized industrial supplies? Contact Josef Gases at (416) 658-1212 for reliable welding gas in Toronto and premium food-grade gas delivery right to your shop floor.
Nozzle Wear and Consumable Decay
The torch nozzle shapes the shielding gas column over the weld pool. Worn, clogged, or mismatched front-end consumables ruin gas distribution and trigger instant porosity.
- Clean spatter build-up regularly: Metal droplets stuck inside the nozzle disrupt smooth gas flow into irregular, chaotic currents. Scrape internal walls frequently using dedicated nozzle pliers.
- Replace damaged gas diffusers: Cracked or clogged diffusers send uneven gas pressure out of torch ports. Swap out worn diffusers during routine consumable teardowns.
- Inspect nozzle interior shape: Heat deformation turns round nozzle openings into oval shapes over extended production runs. Replace warped nozzles to keep gas coverage uniform.
- Select correct nozzle orifice sizes: Narrow nozzles restrict gas output over wide joint grooves, while oversized options waste expensive supply. Match nozzle diameters to joint geometry and wire size.
- Maintain correct contact tip recessed depths: A tip extending past the nozzle rim exposes the arc to ambient room air. Set contact tips flush or slightly recessed based on your process.
- Upgrade worn torch components: Old torches with damaged threads or bent necks let air mix into the gas path. Sourcing commercial welding equipment in Toronto keeps your gear performing without gas leaks.
Shop Drafts and Environmental Currents
Even perfect gas settings fail when ambient air currents blow past your torch. Drafts moving faster than four kilometers per hour sweep away shielding cover instantly.
- Set up flexible wind screens: Mobile welding curtains block cross-drafts from open bay doors or overhead fans. Enclose your workspace whenever air movement picks up.
- Redirect cooling fan placements: Shop fans pointed at the operator often blow away gas shielding before it touches metal. Angle air movers away from active welding zones.
- Block overhead HVAC air flow: Ceiling vents positioned directly above welding stations send strong air currents straight down. Install deflectors on vents to divert air away from workspace tables.
- Seal structural workshop gaps: Cold air entering under dock doors or through wall cracks creates persistent floor-level drafts. Weather-strip bay doors to keep indoor air current steady.
- Adjust travel angles in windy spots: Dragging the torch provides better gas coverage in breezy conditions than pushing it. Angle torch heads slightly to shield molten metal from air currents.
- Monitor outdoor field conditions: Outdoor fabrication needs portable tent shelters to maintain clear gas pockets around field joints. Never strike an arc outdoors without physical wind barriers.
Upgrading your shop setup with high-grade torches, regulators, and protective accessories prevents draft-related rework. Call Josef Gases at (416) 658-1212 to order reliable welding equipment in Toronto today.
Contaminated Materials and Base Metal Care
Porosity often starts directly on the metal surface. Oils, mill scale, moisture, and chemical residues release hydrogen gas when hit by the high heat of the welding arc.
- Remove mill scale completely: Thick oxide layers on hot-rolled steel trap moisture and release oxygen into the liquid weld metal. Grind base metal edges down to bright steel before joining.
- Degrease oily steel stock: Machining oils and rust inhibitors vaporize instantly under arc temperatures, creating internal gas bubbles. Clean joints with residue-free solvent before striking an arc.
- Strip paints and coatings: Galvanized coatings, primers, and paints generate heavy fumes and gas pockets inside cooling metal. Grind away all surface coatings at least two inches back from joints.
- Bake damp filler wires: Moisture hanging on stick electrodes or submerged arc fluxes releases hydrogen into the puddle. Store filler materials in heated rod ovens to prevent moisture pickup.
- Clean stainless wire brushes: Using carbon steel brushes on stainless steel leaves tiny iron particles that rust and cause porosity. Keep dedicated stainless brushes for non-ferrous metals.
- Store consumables in dry spaces: Unopened wire spools left on cold concrete floors pick up condensation overnight. Keep all filler metals in warm, dry storage cabinets off the ground.
Advanced Gas Selection and Supply Consistency
Choosing the right gas mixture for specific metals prevents chemical reactions that produce gas pockets. Pure gases and specialty blends perform vastly different functions.
- Use argon-helium for thick sections: High heat conductivity from helium keeps aluminum pools fluid longer, giving trapped hydrogen gas time to escape. Use helium blends on heavy plate joints.
- Switch to argon-oxygen for stainless steel: Adding one to two percent oxygen stabilizes the arc and improves wetting on stainless joints without causing heavy porosity.
- Verify high supply purity standards: Low-grade gas cylinders containing trace moisture or hydrocarbon leaks ruin weld quality across entire shifts. Source high-purity industrial gas cylinders from certified gas distributors.
- Match flow rates to travel speed: Moving the torch faster requires higher gas flow rates to shield the longer molten tail behind the arc. Adjust gas output when increasing travel speeds.
- Use trailing shields on reactive metals: Metals like titanium absorb atmospheric gases at elevated temperatures well after the main torch passes. Attach trailing gas shields to protect cooling metal.
- Select food-grade options for processing gear: Stainless steel food handling equipment requires pristine back-purging gas to prevent sugar-bounding oxidation inside pipes. Utilizing certified food-grade gas guarantees clean, sanitary root passes.
Porous welds waste time, ruin expensive stock, and compromise structural integrity under Canadian fabrication standards. Eliminating porosity requires constant attention to gas delivery systems, torch maintenance, shop air currents, base metal cleanliness, and gas selection. By checking for regulator surges, clearing spatter from nozzles, erecting wind screens, and using pure shielding gases, you eliminate trapped air pockets and produce clean, high-strength weld beads consistently.
Partnering with an experienced supplier makes maintaining top weld quality simple. Josef Gases supplies local operations with premium welding gas in Toronto, high-grade food-grade gas for specialty processing, and durable welding equipment in Toronto. Contact their team of experts today at (416) 658-1212 to streamline your gas delivery, upgrade your shop hardware, and keep your welding operations running smoothly.