Package Price:
$317.00/10lb tubeUsually ships within 3-5 business days
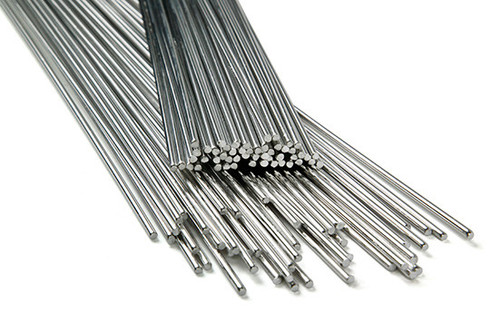
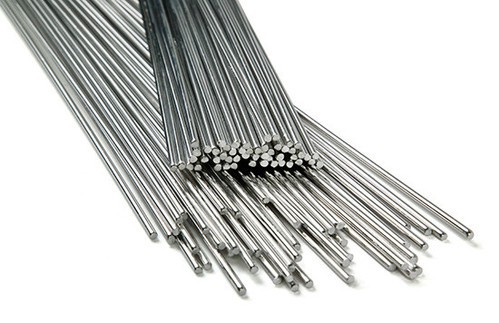
The Exocor ER4130 TIG Welding Rod is a premium low-alloy steel filler metal designed specifically for the Gas Tungsten Arc Welding (GTAW) of AISI 4130 and 4140 base materials. This 3/32-inch diameter rod is formulated with a precise balance of Chromium (approx. 0.80-1.10%) and Molybdenum (approx. 0.15-0.25%), ensuring that the weld deposit exhibits mechanical properties and chemical composition virtually identical to the base metal. This chemical matching is critical for applications where the finished assembly will undergo post-weld heat treatment (PWHT), such as normalizing, quenching, and tempering. Unlike mild steel fillers (e.g., ER70S-2) which do not harden significantly, ER4130 responds to heat treatment, maintaining uniform hardness and tensile strength across the weldment.
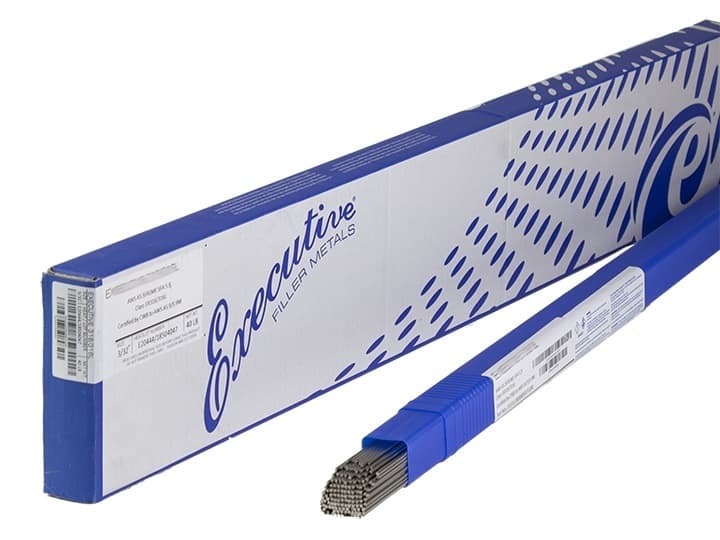
In the as-welded condition, the hardness of the ER4130 deposit is typically higher than that of the base metal, necessitating careful control of cooling rates to prevent brittleness in the heat-affected zone (HAZ). Pre-heating the base material to approximately 300°F - 400°F (depending on material thickness) is standard procedure to mitigate cracking risks. This filler metal is widely utilized in industries demanding high strength-to-weight ratios, including aerospace structural components, motorsports chassis fabrication, and pressure vessels. The rods are supplied in 36-inch cut lengths, cleaned and packaged in 10lb tubes to prevent contamination and oxidation prior to use.
When welding 4130 steel, the choice of filler metal dictates the post-weld processing. If the component is not going to be heat treated, an ER70S-2 or ER80S-D2 rod is often preferred for its ductility. However, for critical assemblies requiring the full strength potential of the 4130 alloy—or where the part will be hardened—ER4130 is the mandatory specification. Users must adhere to strict interpass temperature controls and often employ a slow cooling process (such as burying in sand or wrapping in thermal blankets) to prevent the formation of martensite in the HAZ before the final heat treatment cycle.
| Additional Information |
|---|
| Packaging Description:10lb tube |
| Weld Process:TIG |
| Grade:chrome-moly, NA |
| Packaging:10lb tube, 10lb-tube |
| Brand:Exocor |
| Diameter:2.5mm, 3/32" |
| Position:n/a |
| Polarity:NA |
| AWS Classification:ER4130 |
| Material Composition:Chrome-Moly Steel |
| Rod Length:36" |
| Shielding Gas Requirement:100% Argon |
| Tensile Strength:Approx. 90,000 - 110,000 PSI (Heat Treated) |